- PROFESSIONAL MECHANICAL EQUIPMENT COMPONENT SUPPLIER -

Views: 0 Author: Site Editor Publish Time: 2026-10-22 Origin: Site

Weak welds cost heavy industries millions every single year. Why? Fusing thick alloys requires far more robust thermal management than standard tools can deliver. Improper equipment selection causes severe safety risks. It also triggers cascading production bottlenecks. In this guide, we dive deep into the complexities of reliable equipment selection. We will guide procurement teams and facility managers toward optimal solutions for heavy-duty fabrication.
Carbon steel remains the undisputed backbone of industrial manufacturing. Walk into any bustling shipyard or structural steel plant. You will see this material utilized in massive crane booms and high-pressure vessel housings. Its widespread adoption stems from exceptional tensile strength and impact resistance. Furthermore, it offers undeniable cost-effectiveness. Is all carbon steel metallurgically identical? Absolutely not. Its specific chemical composition directly dictates the required thermal approach.
Generally, this vital material is categorized into three distinct groups based on its carbon content. Low carbon steel, containing up to 0.30 percent carbon, is highly weldable and ductile. It rarely requires pre-heating, making it the absolute standard for high-volume manufacturing environments. Medium carbon steel offers substantially higher strength with a carbon footprint of 0.30 to 0.60 percent. In contrast, it is far more prone to cracking during rapid heating and cooling cycles. Pre-heating and controlled post-weld cooling are often mandatory here. High carbon steel is incredibly tough but notoriously difficult to fuse. It demands strict thermal management protocols to prevent the formation of brittle martensite in the heat-affected zone.
Achieving deep, defect-free root penetration is critical for heavy-duty applications involving thick plates and structural beams. This level of penetration demands precise thermal input and sustained high power output. Selecting industrial-grade Carbon Steel Welding machines ensures that the arc remains stable enough to fuse dense sections continuously. This entirely avoids catastrophic lack-of-fusion defects or excessive porosity.
Selecting the correct core process sets the foundation for an efficient manufacturing cell. Different methodologies offer wildly varying deposition rates and penetration depths. Imagine an operator trying to lay a clean bead on a 1-inch thick structural beam while fighting a crosswind. The chosen process dictates whether that joint passes ultrasonic testing or fails miserably.
Metal Inert Gas Welding utilizes a continuous solid wire electrode paired with an external shielding gas. It offers blistering travel speeds and excellent deposition rates. Post-weld cleanup time is drastically reduced because it produces minimal slag. Furthermore, it is highly adaptable to robotic automation. On the downside, reliance on shielding gas makes it highly vulnerable in drafty environments where gas dispersion instantly leads to severe porosity.
Flux-Cored Arc Welding is widely considered the heavyweight champion for thick plate fabrication. It utilizes a tubular wire filled with proprietary flux compounds. These compounds generate their own shielding gas and lay down a protective slag layer over the molten puddle. This process delivers unparalleled penetration and exceptionally high deposition rates, often exceeding 10 pounds of metal per hour. It excels in outdoor structural environments and effortlessly burns through surface rust.
Tungsten Inert Gas Welding relies on a non-consumable tungsten electrode. It provides ultimate precision and produces clean, x-ray quality aesthetics. However, it is an agonizingly slow process. In the realm of heavy-duty manufacturing, this method is typically reserved exclusively for critical root passes in high-pressure pipe joining.
Shielded Metal Arc Welding uses a consumable flux-coated electrode. It is highly portable and completely unaffected by wind. While it remains the gold standard for rugged outdoor field repairs, its slow manual nature makes it highly inefficient for high-volume factory production.
| Process | Deposition Rate | Penetration Depth | Ideal Environment |
|---|---|---|---|
| MIG | High | Medium | Indoor / Automated Cells |
| FCAW | Very High | Deep | Outdoor / Heavy Structural |
| TIG | Low | Precise / Controlled | Clean Rooms / Pipe Roots |
| Stick | Low to Medium | Variable | Field Maintenance / Muddy Sites |
Procurement managers must aggressively look beyond glossy marketing brochures. The focus must remain on the hard technical parameters. These metrics dictate a machine's true capability to survive grueling industrial workloads.
The fundamental rule of thumb in heavy fabrication requires approximately 1 amp of output power for every 0.001 inch of material thickness. Therefore, fusing a half-inch solid plate effectively requires a machine capable of producing up to 500 amps for a single-pass weld. Heavy-duty manufacturing facilities typically require Carbon Steel Welding machines with a maximum output ranging from 300 to well over 600 amps to maintain profitable production speeds.
Duty cycle is arguably the most critical operational metric on the factory floor. It represents the percentage of a 10-minute period that a unit can operate continuously before its internal thermal sensors force a shutdown. A machine with a 30 percent duty cycle at 300 amps can only run for 3 minutes before demanding 7 minutes of rest. In a high-stakes manufacturing environment, a low duty cycle creates unacceptable bottlenecks. Industrial applications absolutely require machines engineered with a 60 to 100 percent duty cycle at high amperages.
Recent market data highlights a massive shift in industry trends. There is a pronounced acceleration toward energy-efficient, smart inverter technologies. As global sustainability mandates tighten and energy costs soar, modern manufacturing facilities are rapidly transitioning away from power-hungry transformer units. The integration of IoT sensors now allows real-time monitoring of arc stability and energy consumption. Furthermore, standard single-phase power is entirely insufficient. True industrial operations demand 3-phase power, typically 480V or 575V. This provides a continuous flow of electricity, drastically reducing spatter and sustaining the thermal output necessary for massive steel structures.
The landscape of metal fabrication is rapidly evolving. Transitioning to highly sophisticated microprocessor-controlled equipment allows facility engineers to maximize throughput. It simultaneously drives down defect rates.
In traditional analog setups, operators were forced to manually balance voltage and wire feed speed. This was a tedious trial-and-error process. Modern digital systems leverage synergic controls instead. The user simply inputs the material type, shielding gas composition, and wire diameter into an intuitive interface. The internal algorithms dynamically calculate and lock in the optimal voltage curve, ensuring absolute standardization across multiple shift changes.
Managing heat input is a critical metallurgical concern when manipulating medium to high carbon alloys. Digital machines equipped with pulsed technology alternate rapidly between a high peak current and a low background current. The peak current pinches off the wire droplet to ensure deep penetration. The background current keeps the puddle fluid without adding excessive heat. This digital precision virtually eliminates spatter, cutting down brutal post-weld grinding labor by up to 80 percent.
Industry 4.0 has firmly planted its roots in heavy manufacturing. High-end digital units now feature industrial Ethernet connectivity. Production managers can monitor arc-on time, consumable usage, and specific parameter deviations in real-time. These digital power sources integrate seamlessly if your facility utilizes robotic arms. They provide the ultra-low latency communication required for high-volume automated cells.
A frequent pitfall in industrial procurement is attempting to deploy prosumer equipment to save on initial capital expenditures. Deploying retail-grade equipment in a heavy-duty environment inevitably leads to catastrophic premature failure.
True industrial equipment is over-engineered to survive harsh factory environments. Standard units often utilize cheap aluminum transformers and plastic wire drive housings. In contrast, heavy-duty Carbon Steel Welding machines feature heavy-gauge copper windings and dust-proof IP23-rated circuit boards. Commercial units employ robust 4-roll cast aluminum drive systems. This ensures uninterrupted feeding even when pushing heavy 60-pound spools of stiff flux-cored wire through 15-foot torch cables.
Generating sustained power creates immense heat at the torch head. Standard gas-cooled torches rely solely on ambient air and shielding gas flow to dissipate this heat. They will quickly overheat in a continuous production environment, destroying consumables and burning the operator's hands. Heavy-duty manufacturing mandates water-cooled systems. These utilize a dedicated radiator and pump to circulate coolant directly through the torch neck, allowing operators to work comfortably at 100 percent duty cycles.
A premium industrial machine may demand a higher initial investment. However, its Total Cost of Ownership is exponentially lower than continuously replacing retail units. Cheaper machines suffer from burnt-out motherboards and trigger massive labor losses due to low duty cycles. Unplanned downtime can exceed thousands of dollars per hour in a commercial plant. Investing in commercial-grade equipment guarantees high uptime and predictable joint quality.
Follow this objective evaluation framework before issuing a purchase order to streamline your procurement process and protect your capital investment.
Assess Material Thickness and Penetration Requirements: Audit your engineering drawings. Identify the maximum thickness processed daily and apply the 1 amp per 0.001 inch rule to determine your absolute baseline amperage requirement.
Determine Your Production Volume and Duty Cycle: Evaluate your true arc-on time. Prioritize machines offering a 100 percent duty cycle at your required operating amperage if operators are running continuous long seams.
Evaluate the Work Environment: High-amperage digital MIG systems are optimal for strictly indoor controlled shop environments. Conversely, open shipyards or drafty structural yards demand rugged FCAW-optimized equipment.
Check Facility Power Availability: Consult with your facility engineer. Verify that your electrical infrastructure can comfortably supply the clean 3-phase power demanded by heavy industrial assets.
Test for Ergonomics and Usability: Operator fatigue directly correlates with defect rates. Consider separate wire feeders mounted on boom arms to drastically reduce the lifting and dragging required by the workforce.
Maintaining in-house manufacturing is not always the most financially viable solution for every single component. Procurement teams must regularly conduct rigorous Make vs. Buy analyses.
Purchasing top-tier robotic cells, hiring certified metallurgists, and maintaining expensive non-destructive testing equipment requires massive capital overhead. The return on investment for purchasing dedicated equipment will likely be negative if your facility only occasionally requires highly complex structural nodes or parts requiring strict post-weld stress relief.
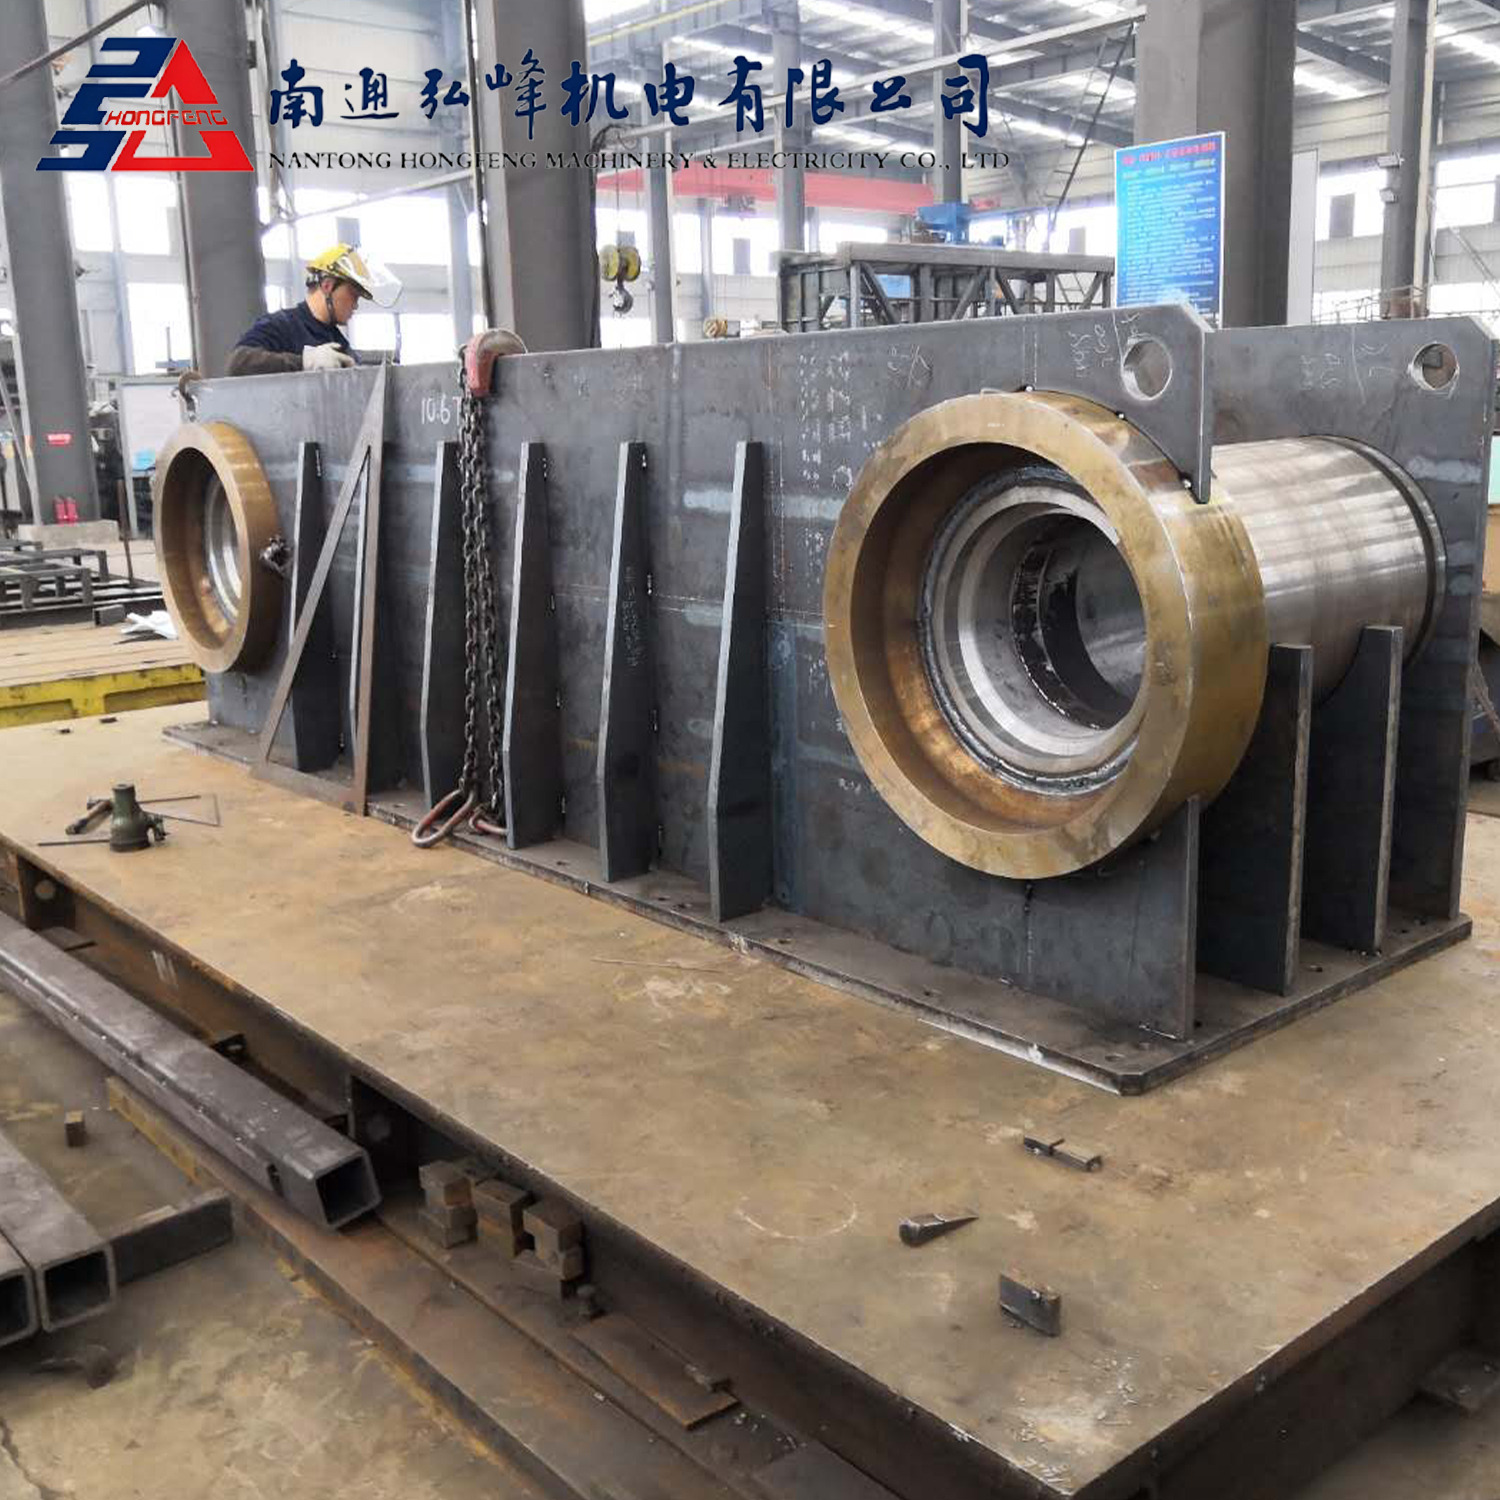
Consider the fabrication of heavy machinery sub-assemblies that face extreme dynamic loads. Outsourcing is often the strategically superior move. By utilizing professional fabrication partners equipped with advanced Carbon Steel Welding machines, manufacturers can instantly leverage the expertise of dedicated fabrication shops. These external partners already possess the heavy-duty power sources and ISO-certified quality control protocols required to deliver defect-free components on time.
Apply the same rigor used for equipment purchases when evaluating an outsourced fabrication partner. Demand documented proof of AWS certifications. Inspect their capacity for internal ultrasonic testing, and ensure they have a verifiable history of processing heavy-duty alloys to exact engineering tolerances.
Choosing the correct industrial equipment requires a highly technical evaluation of your facility's daily demands. You must meticulously balance duty cycles with maximum output power, ensuring the specific process matches your environmental realities. Furthermore, embracing modern digital technologies can drastically reduce defect rates and labor costs. Yet, it is equally important to recognize when internal fabrication is inefficient. Outsourcing highly complex specialized parts to proven experts can preserve capital, mitigate risk, and drastically improve overall component quality.
Ready to upgrade your manufacturing capabilities? Whether you are configuring a new production cell or seeking reliable outsourced fabrication, proper equipment is non-negotiable. Explore high-performance solutions and professional services at Hongfeng Machine to ensure your heavy-duty projects are executed with absolute precision and long-term profitability.
Flux-Cored Arc Welding and high-amperage Metal Inert Gas welding are generally the most effective processes for thick heavy-duty materials. Flux-Cored is particularly favored for structural applications because the flux provides incredibly deep penetration and allows for massive deposition rates, even in outdoor environments. High-amperage MIG is excellent for indoor high-speed manufacturing where robotic or semi-automated processes are utilized.
A water-cooled system is highly recommended if your manufacturing process requires operators to work continuously at over 250 to 300 amps. Heavy-duty fabrication requires significant sustained heat input for proper joint penetration. A water-cooled torch efficiently dissipates this intense heat, extending the lifespan of your contact tips and significantly reducing operator fatigue.
For heavy carbon steel fabrication using the MIG process, a mixture of 75 to 90 percent Argon and 10 to 25 percent Carbon Dioxide is typically the industry standard. Higher argon content provides a smoother arc and less spatter, while the addition of CO2 increases heat input, ensuring deeper root penetration on thick plates.
Pre-heating is absolutely critical when working with thick plates or medium-to-high carbon alloys. It slows down the cooling rate of the molten puddle and the surrounding heat-affected zone. This slow cooling process allows trapped hydrogen to escape, drastically reducing the risk of hydrogen-induced cold cracking and preventing the steel from becoming excessively brittle.
Duty cycle dictates how many minutes out of a standard 10-minute timeframe a power source can operate continuously at a given amperage before it must actively cool down. A low duty cycle creates severe costly production bottlenecks in industrial environments. High-volume manufacturing requires machines with 60 to 100 percent duty cycles to ensure uninterrupted operation and maximum labor efficiency.